Sustainable and intelligent technologies for efficient beverage production
November 18, 2026 (Heidelberg, Germany) — Under the motto “Smart Technologies for Better Beverages”, ProMinent presented innovative solutions for sustainable, safe and efficient beverage production at BrauBeviale 2026 in Nuremberg. The focus of the exhibition stand was on technologies for water treatment, disinfection and dosing, as well as intelligent measurement, control and sensor technology for reliable process monitoring.
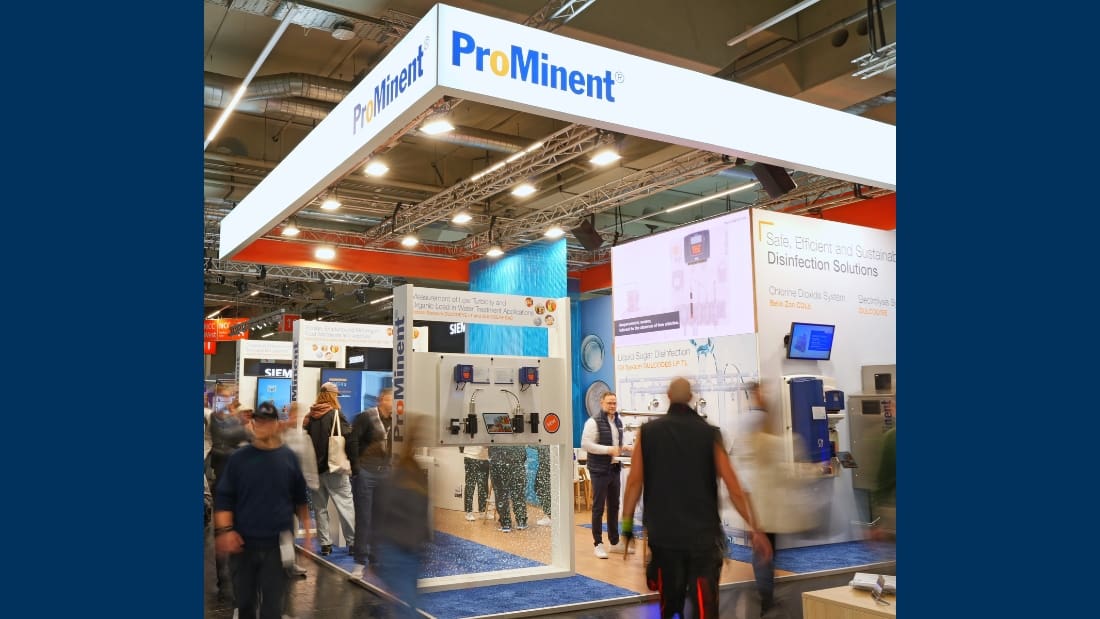
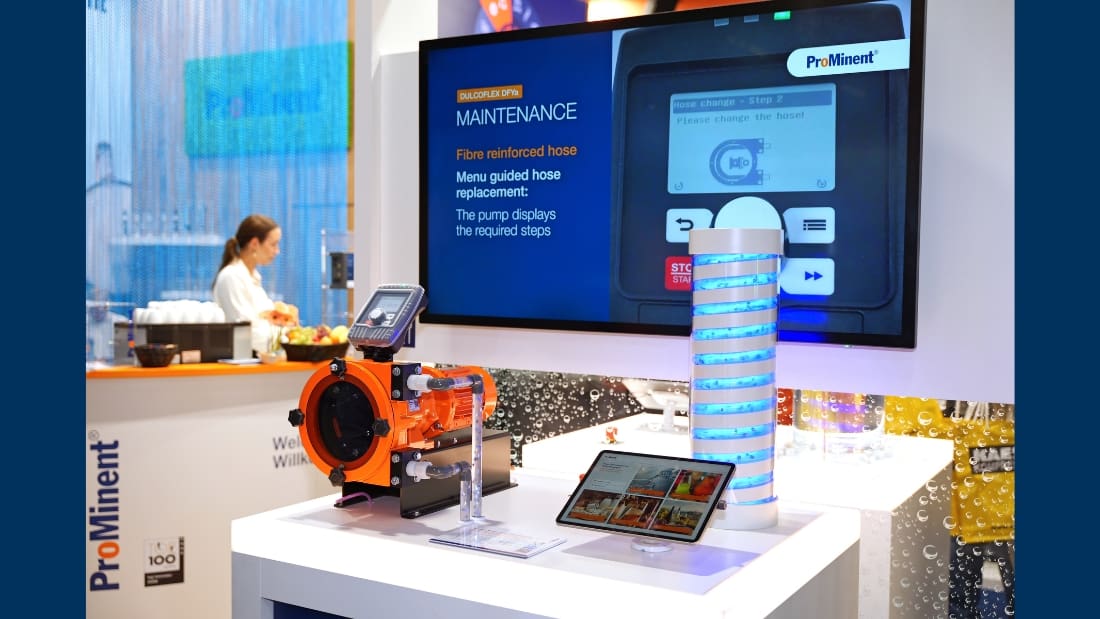
In 2026, BrauBeviale once again underlined its importance as the key meeting place for the European drinks industry. Around 27,000 trade visitors came to Nuremberg from 10 to 12 November. More than 800 exhibitors from 38 countries presented solutions covering the entire process chain, with almost half of them coming from abroad. 93 per cent of trade visitors came from Europe.
At the ProMinent stand, too, there was keen interest in concrete, practical solutions to current challenges in beverage production. Discussions focused in particular on reliable water treatment, hygienic dosing, energy and resource efficiency, and the continuous monitoring and automation of production processes.
“BrauBeviale has once again demonstrated that beverage manufacturers are seeking solutions that combine sustainability, process reliability and cost-effectiveness. In particular, the interest in intelligent water treatment, hygienic dosing technology and in-line process monitoring confirms our commitment to consistently developing these areas further. At the same time, regulatory requirements are increasing, for example with regard to Regulation (EC) No 1935/2004 on materials intended to come into contact with food. Our customers are therefore increasingly looking for a reliable partner who not only guarantees innovative technologies and regulatory compliance, but also offers comprehensive services from a single source. Through professional installation, commissioning and regular maintenance, we make a significant contribution to high system availability, thereby supporting safe working conditions, stable production processes and consistently high food and product quality. At the same time, we help our customers to use resources efficiently and optimise their operating costs in a sustainable manner.” — Moritz Buck, Managing Director of ProMinent Deutschland GmbH
Energy-efficient disinfection of liquid sugar
One of the particular highlights of the trade fair was the DULCODES LP TL UV system. It was developed specifically for the disinfection of sugar syrup and enables the reliable inactivation of heat-resistant germs. It therefore represents an energy-efficient alternative to conventional heat pasteurisation.
The DULCODES LP TL operates with VARIO-Flux high-performance amalgam lamps featuring dynamic lamp heating. In conjunction with the optimised flow pattern in the thin-film reactors, a homogeneous UV dose is achieved. This enables efficient disinfection even with viscous media with low UV transmission. By eliminating the need for thermal treatment, energy savings can be combined with gentle product handling.
Thermoresistant spores can be eliminated by 99.99 per cent using the DULCODES LP TL. At the same time, the quality, taste, appearance and aroma of the sugar syrup remain unaffected. For beverage manufacturers, the system thus offers a reliable solution for combining high product safety with energy- and cost-efficient operation.
Precise dosing for the highest hygiene standards
Another key focus was on solutions for the precise and hygienic dosing of food ingredients and additives. With the DULCODOS Compact F&B, ProMinent presented a dosing system specifically designed for applications involving direct food contact. It supports beverage manufacturers in the reliable dosing of flavourings, additives and other process media.
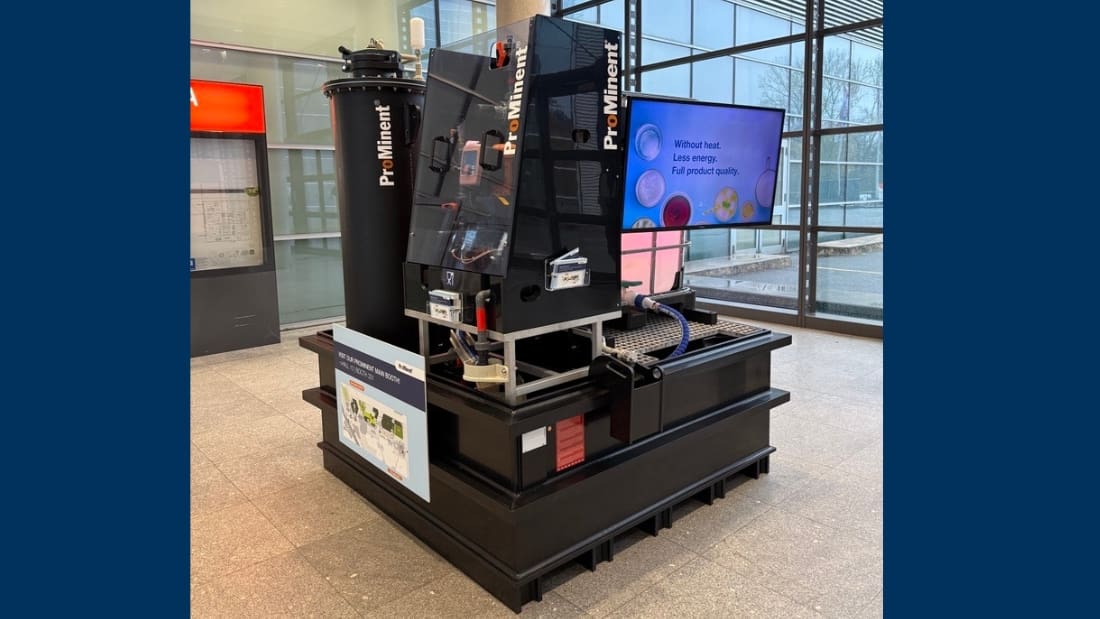
The portfolio was complemented by the DULCODOS SAFE-IBC F&B. This dosing and emptying station enables the safe emptying of IBC containers whilst simultaneously ensuring the continuous and precise dosing of food additives. A dead-space-free design, CIP capability and food-grade materials ensure compliance with stringent hygiene and process safety requirements. Even in the entrance area of the trade fair, the full-scale DULCODOS SAFE-IBC F&B attracted a great deal of attention. The life-size, real-world system was a particular highlight and offered visitors the opportunity to experience the solution at close quarters.
Intelligent process monitoring in water treatment
Intelligent monitoring of water quality also offers great potential for more efficient beverage production. ProMinent presented the DULCOMETER diaLog C measurement and control unit for this purpose, as well as the sensor solutions DULCOEYE LT, DULCOEYE SAC and DULCOTEST SurfaceGuard.
The DULCOEYE LT was developed specifically for measuring low turbidity levels and enables the continuous monitoring of drinking water, product water and process water. Automatic calibration and integrated self-cleaning ensure stable measurement results with minimal maintenance. The DULCOEYE SAC optical sensor also detects organic loads via the spectral absorption coefficient and can derive further relevant parameters, such as chemical oxygen demand, from this.
When used in conjunction with the DULCOMETER diaLog C, measurement data is processed directly and dosing is adjusted automatically. This enables plants to respond to changes in water quality whilst being operated cost-effectively.
With the DULCOTEST SurfaceGuard, ProMinent also presented a solution for the continuous monitoring of plant surfaces. The system detects both biofilms and inorganic deposits at an early stage. Cleaning and dosing measures can thus be controlled more effectively according to need, and chemical usage reduced.
Practical solutions meet specific requirements
Under the theme ‘Time for Opportunities’, BrauBeviale 2026 highlighted solutions for the drinks industry that can be implemented immediately. The spectrum ranged from more flexible production concepts and energy and resource efficiency to water treatment and process optimisation.
ProMinent’s exhibition stand tied in perfectly with this theme: featuring technologies that help beverage manufacturers use water, energy and chemicals more efficiently, monitor processes reliably and, at the same time, meet high standards of hygiene and product quality.
The positive response at BrauBeviale 2026 confirms the focus of the ProMinent portfolio: Smart Technologies for Better Beverages.
About ProMinent
The ProMinent Group is a manufacturer of components and systems for metering technology as well as a reliable solutions partner for water treatment and digital fluid management. The group’s headquarters are located in Heidelberg. More than 3,100 employees in around 50 of its own sales and service companies, as well as 12 production sites, work every day to offer ProMinent customers customized solutions and the usual competent service.
More information: www.prominent.com